Top 10 Instrument Finishing Craftsmanship Types to Source

Choosing the right finish can change an instrument’s appearance, durability, tone, and perceived value. This guide explores the Top 10 Instrument Finishing Craftsmanship Types to Source, from hand-rubbed oil finishes to high-gloss lacquer, natural wax, metallic plating, and carefully aged surfaces.

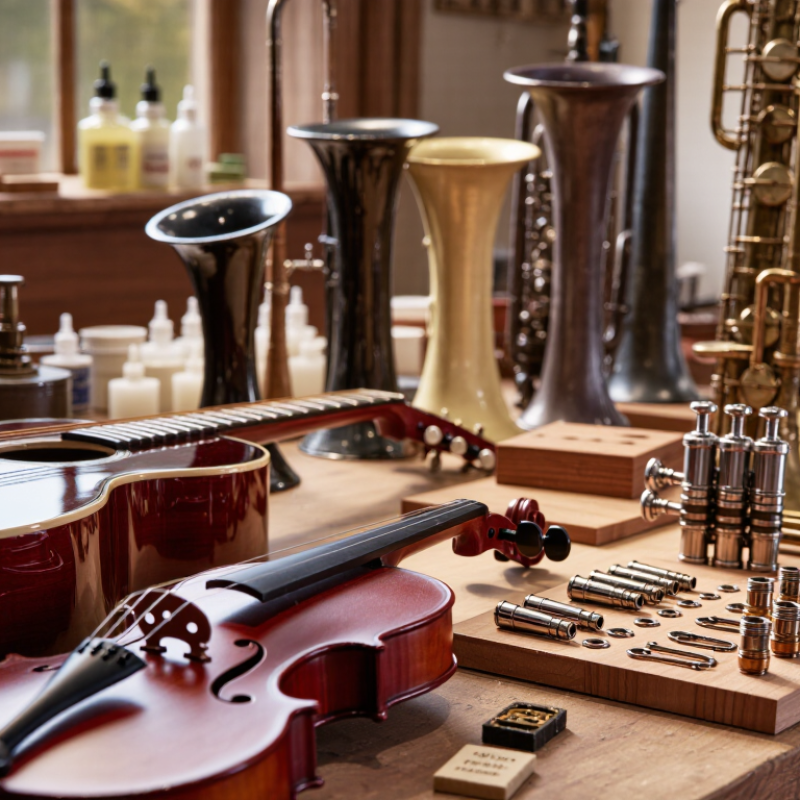
Each method leaves visible evidence of the maker’s skill. A lacquered guitar may show a deep, glass-like reflection under workshop lights. A hand-oiled violin can reveal warm wood grain beneath a soft satin surface. Metal components may require even plating, clean edges, and stable color across curved areas. These details matter during supplier evaluation.

Sourcing should involve more than attractive sample photos. Ask about substrate preparation, coating thickness, curing time, environmental controls, repair options, and batch consistency. Experienced suppliers should provide material specifications, process records, inspection images, and relevant testing information. Small samples can expose major problems, including uneven gloss, trapped dust, sharp coating transitions, or premature cracking.

No finish is perfect. That matters.

A durable coating may hide natural texture. A delicate finish may require more careful handling. Historical accuracy can also conflict with modern production efficiency. I have found that the best choice depends on the instrument’s materials, playing environment, target price, and expected service life. This article compares ten craftsmanship types with practical sourcing considerations, helping buyers identify skilled workshops and avoid vague quality claims. Verify every critical detail before approving production. Even a beautiful prototype can fail after repeated handling.

Top 10 Instrument Finishing Craftsmanship Types to Source

Define the Top 10 Instrument Finishes by Process, Material, and Function

Instrument finishing should be defined by process, material, and function, not appearance alone. These ten craftsmanship types cover common sourcing needs.

Lacquer creates a smooth protective film and supports vivid colors. Oil finishing penetrates wood, emphasizing grain with a softer sheen. Wax adds warmth, but it offers limited resistance to moisture.

Shellac dries quickly and gives wood a clear, traditional surface. Powder coating uses charged polymer particles and heat for durable metal coverage. Anodizing changes the outer layer of aluminum and improves surface hardness.

Plating deposits a thin metal layer for corrosion protection and visual contrast. Ceramic coating resists heat and surface wear in demanding environments.

Patina finishing uses controlled chemical reactions to create an aged appearance. Hand-rubbed finishing builds subtle depth through repeated manual polishing.

Tips: Request process records, material specifications, and sample panels. Check color under warm and cool light. Test edges, threads, and contact points. A flawless sample can still hide weak adhesion. I have seen finishes fail around sharp corners first. Ask how the surface performs after cleaning, friction, and temperature changes. Do not judge quality by gloss alone. The best finish depends on the instrument’s material, handling frequency, storage conditions, and repair requirements. Some workshops may describe a coating as “premium” without providing measurable data. That deserves a second look. Ask for thickness ranges, curing conditions, inspection methods, and acceptable color variation before placing an order.

Compare Surface Roughness Targets from Ra 0.8 to 3.2 µm

Top 10 Instrument Finishing Craftsmanship Types to Source

Compare Surface Roughness Targets from Ra 0.8 to 3.2 µm

Surface roughness affects cleaning, grip, wear, and measurement stability. Ra 0.8 µm usually requires precision grinding, honing, lapping, or fine polishing. These methods can produce smooth contact areas for instrument fittings and moving components. Measure it.

Ra 1.6 µm often suits fine grinding, brushing, controlled polishing, and light vibratory finishing. It offers a practical balance between appearance and production cost. Ra 3.2 µm may come from standard grinding, bead blasting, barrel tumbling, or heavier brushing. These finishes can hide minor marks, but they may retain abrasive particles or uneven edges. Do not guess.

The ten options deserve different inspection controls: precision grinding, fine grinding, lapping, honing, polishing, vibratory finishing, barrel tumbling, bead blasting, brushing, and electropolishing. Electropolishing can improve cleanability, yet it may change dimensions on sharp features. A supplier should report the instrument, cutoff length, sampling location, and measurement direction. A single Ra value is not enough. Surface texture can vary near welds, corners, holes, and clamped areas. I have seen attractive parts fail because roughness was checked only on a flat center zone. Define acceptance areas on the drawing, then compare test coupons made from the same material and process. The target may need revision after assembly trials. Something can be technically compliant and still feel wrong in use.

Assess Plating Thickness, Adhesion, and Wear Resistance by Finish Type

Top 10 Instrument Finishing Craftsmanship Types to Source

When sourcing instrument finishes, assess thickness, adhesion, and wear resistance together. A thicker coating is not automatically better. Electroless nickel and hard chrome often provide strong wear resistance, but excessive thickness can affect tight assemblies. Nickel-chrome finishes require careful layer control. Use X-ray fluorescence testing for non-destructive thickness checks, then confirm critical areas with cross-sectional analysis when necessary.

Anodized aluminum offers a hard, integrated surface with minimal dimensional change. Its color layer may fade under abrasion. Powder coating provides a thicker protective film, but edge coverage and curing quality require close inspection. PVD coatings are usually thin and highly wear resistant, although poor substrate preparation can cause early delamination. Black oxide and phosphate finishes add limited thickness. They depend heavily on sealing and the service environment.

Test adhesion on representative parts, not only flat coupons. Pull-off, cross-hatch, and scratch testing reveal different weaknesses. Inspect contact points, threads, corners, and grip surfaces after simulated handling cycles. Stainless surfaces may require controlled pretreatment before plating. This is where suppliers sometimes overstate performance. Ask for measured values, test conditions, and failure photographs. A result without method details is difficult to trust. I have found that visual uniformity can mislead; a bright surface may still have weak adhesion beneath it. Recheck the specification after production changes.

Match Each Finish to Corrosion Requirements Using ISO 9227 Testing

Top 10 Instrument Finishing Craftsmanship Types to Source

Match each finish to corrosion requirements using ISO 9227 testing. The right finish begins with the instrument’s exposure, substrate, and maintenance routine.

Common options include:

electropolishing passivation anodizing powder coating wet painting nickel plating chromium plating zinc plating PVD coating black oxide

Each method changes surface chemistry, hardness, appearance, and repairability.

ISO 9227:2022 defines neutral salt spray, acetic acid salt spray, and copper-accelerated acetic acid salt spray procedures. It does not set universal pass or fail limits. Buyers must specify exposure hours and defect limits with suppliers.

That detail matters. Salt mist entering a scratched edge can reveal weak pretreatment quickly. A clean panel may still hide seam corrosion.

NACE’s IMPACT study estimated global corrosion costs at approximately US$2.5 trillion annually, equal to 3.4% of global GDP. The report also identified corrosion control and better practices as major savings opportunities.

For mild indoor exposure, passivation or anodizing may provide practical protection. Marine or chloride-heavy environments often need sealed anodizing, robust plating, or multilayer paint systems. Powder coating looks durable, but damaged edges require careful inspection.

I would not approve a finish from appearance alone.

Test representative assemblies, including welds, fasteners, corners, and machined marks. ISO 9227 results can guide sourcing, but field exposure remains imperfect.

Real instruments face fingerprints, abrasion, cleaning chemicals, and trapped moisture. Those variables deserve a separate review.

Specify Supplier Quality Controls with ISO 2859-1 AQL 1.0 Criteria

Top 10 Instrument Finishing Craftsmanship Types to Source

Specify Supplier Quality Controls with ISO 2859-1 AQL 1.0 Criteria

Instrument finishing requires more than a bright surface. Check polishing, brushing, plating, anodizing, laser marking, passivation, bead blasting, knurling, engraving, and protective coating. In practical supplier audits, I inspect under 500–1,000 lux lighting. I also rotate each part to expose drag marks, uneven color, burrs, and blurred graduations. Small defects often hide near edges and threaded areas.

ISO 2859-1 AQL 1.0 provides a disciplined sampling framework, not a promise of zero defects. Under General Inspection Level II, a lot of 3,201–10,000 pieces commonly uses code letter L. That means 200 samples; at AQL 1.0, acceptance may be five defects, with rejection at six. Confirm the exact table edition and lot range before approval. Functional, dimensional, and safety-critical checks still need separate controls.

The ISO Survey 2023 recorded more than 1.2 million ISO 9001 certificates worldwide, showing how widely documented quality systems are used. Yet certification alone cannot verify finishing consistency. Require dated inspection images, coating-thickness readings, surface roughness results, approved reference samples, and corrective-action records. The NIST Engineering Statistics Handbook stresses that sampling decisions involve producer and consumer risks. My own plans have sometimes overtrusted visual inspection. That was a mistake. AQL 1.0 should guide supplier release, while trend data and process capability reveal whether the next batch is quietly drifting.

Top 10 Instrument Finishing Craftsmanship Types to Source — Specify Supplier Quality Controls with ISO 2859-1 AQL 1.0 Criteria

No. Finishing Craftsmanship Type Typical Instrument Applications and Materials Required Appearance and Functional Target Supplier Quality Controls Inspection or Test Method ISO 2859-1 AQL 1.0 Purchasing Criteria
1 Mirror Polishing Stainless-steel surgical instruments, optical housings, laboratory tools, and precision handles. Uniform reflective surface with no visible pits, orange peel, grinding lines, embedded abrasive, or edge rounding beyond drawing limits. Define maximum surface roughness, normally Ra ≤ 0.20 µm where a highly reflective surface is required; control abrasive sequence, polishing pressure, heat buildup, edge protection, and final cleaning. Visual inspection under controlled diffuse light; calibrated surface-roughness tester on representative areas; dimensional check on functional edges and mating features. Use ISO 2859-1 normal single sampling, General Inspection Level II, with the lot-size-dependent code letter. Apply AQL 1.0 to major appearance and workmanship defects; use zero tolerance for safety-critical damage.
2 Satin or Brushed Finishing Stainless-steel instrument bodies, control panels, medical handles, and laboratory enclosures. Consistent directional grain, even gloss, no cross-scratches, torn metal, discoloration, or visible transition lines between adjacent areas. Specify abrasive grade and grain direction; maintain belt or wheel condition; mask non-finish zones; define allowable grain deviation and surface roughness, commonly Ra 0.40–1.60 µm according to the drawing. Visual comparison with an approved master sample under consistent lighting; surface-roughness measurement; check grain direction and masking boundaries. Inspect according to the applicable ISO 2859-1 code letter at AQL 1.0 for major appearance defects. Treat exposed base metal, sharp burrs, and functional-area damage as rejectable defects.
3 Glass-Bead Blasting Stainless steel, aluminum, and titanium instrument housings requiring glare reduction and a uniform matte texture. Even matte appearance and consistent texture without blast shadows, streaks, embedded media, excessive erosion, or masked-area overspray. Control bead size, blasting pressure, nozzle distance, angle, exposure time, and media cleanliness; verify masking of threads, bores, datum surfaces, and sealing faces. Visual inspection against an approved texture panel; roughness measurement; dimensional and thread-gauge checks; inspection for trapped media using cleaning and air-blow procedures. Apply ISO 2859-1 normal inspection at AQL 1.0 for visible nonuniformity and process damage. Critical sealing, threaded, and datum surfaces should be individually verified where specified.
4 Chemical Etching and Passivation Austenitic stainless-steel instruments and components requiring improved corrosion resistance after machining, welding, or polishing. Clean, uniform surface free from scale, free iron, acid stains, residue, and localized attack; corrosion resistance must meet the agreed specification. Control bath chemistry, concentration, temperature, immersion time, rinsing, and drying; maintain chemical records; prevent cross-contamination from carbon-steel tooling. Visual inspection; water-break or cleanliness check; free-iron detection where applicable; corrosion testing such as salt spray or immersion testing only when required by the product specification. Use AQL 1.0 for cosmetic and workmanship defects under ISO 2859-1. Any failed corrosion-resistance or passivation requirement should be treated as a major or critical nonconformity and investigated by lot.
5 Hard Anodizing Aluminum instrument frames, knobs, mounts, housings, and wear surfaces requiring hardness and corrosion protection. Uniform color and coverage, controlled coating thickness, good adhesion, and no burns, powdery areas, pits, bare spots, or rack marks in visible zones. Specify alloy, pretreatment, coating thickness, color tolerance, sealing requirement, contact-point location, and masking limits; record bath temperature, current density, voltage, and process time. Coating-thickness measurement using an appropriate calibrated method; adhesion test when specified; color comparison under standardized lighting; visual inspection and dimensional verification of fits. Inspect under ISO 2859-1 at AQL 1.0 for coating appearance and workmanship. Thickness, adhesion, and critical dimensional requirements should be measured according to the control plan, with failed critical characteristics rejected.
6 PVD Decorative or Wear Coating Stainless-steel or hardened-steel instrument components requiring a thin, hard, wear-resistant, or colored surface. Uniform hue and gloss with complete coverage, strong adhesion, and no pinholes, nodules, arcing marks, flaking, or edge overbuild that affects assembly. Define substrate preparation, coating chemistry or color family, thickness range, masking, rack marks, adhesion requirement, and allowable color variation; monitor chamber cleanliness and batch parameters. Visual inspection; coating-thickness measurement where practical; adhesion testing such as tape or scratch testing when specified; abrasion or wear testing for functional surfaces. Use ISO 2859-1 normal single sampling at AQL 1.0 for visible and workmanship defects. Adhesion failure, exposed substrate in a functional area, or coating delamination should be classified as major defects.
7 Electroplating Nickel, chromium, tin, silver, or gold-plated conductive contacts, connectors, knobs, and corrosion-sensitive instrument parts. Continuous, adherent, and uniform deposit with controlled thickness; no blistering, peeling, burning, nodules, stains, skip plating, or blocked contact areas. Specify deposit type, minimum local thickness, substrate preparation, masking, bath control, rinsing, drying, and contact-area requirements; retain bath-analysis and thickness records. X-ray fluorescence or another suitable thickness method; visual inspection; adhesion test; solderability or contact-resistance testing when required by the application. Apply ISO 2859-1 AQL 1.0 for cosmetic and workmanship defects. Minimum thickness, adhesion, solderability, and electrical performance are functional requirements and should have defined lot controls in addition to visual sampling.
8 Powder-Coat Finishing Aluminum and steel instrument cabinets, frames, mounting brackets, and protective equipment enclosures. Even color, gloss, and film coverage with no runs, craters, fisheyes, orange peel beyond the approved standard, contamination, pinholes, or exposed substrate. Control substrate cleaning, pretreatment, powder batch identification, film thickness, curing temperature and time, grounding, masking, and edge coverage. Visual inspection under controlled lighting; dry-film thickness measurement; cure verification by an approved solvent-rub or equivalent method; adhesion testing when specified. Use ISO 2859-1 General Inspection Level II and AQL 1.0 for major finish defects. Under-cured coating, exposed substrate, and coating that interferes with grounding or assembly should be treated as major defects.
9 Laser Marking and Engraving Serial numbers, graduations, scales, symbols, calibration references, and traceability marks on metal, coated metal, polymer, and glass components. Correct character content, position, contrast, depth, line width, and legibility; no double images, excessive heat discoloration, burrs, or damage to sealing or structural areas. Lock the approved artwork and revision; verify program-to-part matching; control focus, power, speed, frequency, fixturing, and contrast; maintain 100% verification of variable data and serial numbers. First-article verification against the approved drawing or artwork; 100% barcode or character readability check where applicable; visual inspection and dimensional position check. Apply ISO 2859-1 AQL 1.0 to fixed artwork and workmanship defects, but perform 100% verification for unique identification, serial data, safety markings, and legally required information.
10 Precision Knurling and Textured Grip Finishing Metal instrument knobs, adjustment wheels, handles, and manually operated controls made from aluminum, brass, or stainless steel. Uniform diamond or straight pattern, correct pitch and depth, clean termination, adequate grip, and no torn material, crushed peaks, sharp burrs, or eccentricity. Specify knurl form, pitch, major diameter, depth, runout, termination, and allowable tool marks; control tool condition, feed rate, workholding, and burr removal without flattening the pattern. Visual and tactile inspection; optical comparator or profile measurement; pitch and diameter measurement; runout check; functional torque or grip test when specified. Inspect according to ISO 2859-1 at AQL 1.0 for pattern and workmanship defects. Sharp burrs, loose material, incorrect control geometry, or excessive runout affecting operation should be classified as major defects.
Sampling note: ISO 2859-1 does not assign one universal sample quantity. The supplier and buyer must select the lot-size-dependent code letter, inspection level, sampling type, and acceptance/rejection numbers from the applicable ISO 2859-1 table. The criteria above assume normal single sampling, General Inspection Level II, and AQL 1.0 for noncritical major defects. AQL is a lot-based sampling limit, not permission to knowingly ship defective parts; critical safety, identification, sealing, and functional characteristics should be controlled separately, often by 100% inspection or a dedicated process-control plan.