Global manufacturing buyers often manage a chain that stretches from raw materials to finished goods. A delay at one supplier can leave an assembly line waiting, even when every other component is ready. Vertical integration manufacturing offers one way to bring more stages of production under coordinated ownership or control. It can improve visibility and planning, but it does not automatically lower costs or remove risk. That distinction matters.
For buyers, the right approach depends on product complexity, demand stability, supplier capability, and available capital. A factory visit may reveal details that a spreadsheet misses: crowded staging areas, aging equipment, or quality checks recorded on paper. These clues deserve careful review, not quick conclusions. More control can also mean more responsibility for staffing, inventory, maintenance, and consistent quality. Sometimes the better choice is a reliable specialist partner. It depends.
This guide shares seven practical tips for assessing vertical integration across global manufacturing operations. It covers how to map critical processes, compare ownership with supplier partnerships, evaluate total costs, and check operational readiness. Buyers should also examine traceability, production capacity, and contingency plans before changing their sourcing model. No checklist can predict every disruption, and real projects rarely follow a perfect plan. A measured assessment helps teams spot gaps early, ask better questions, and choose an operating model that fits their products and long-term goals.
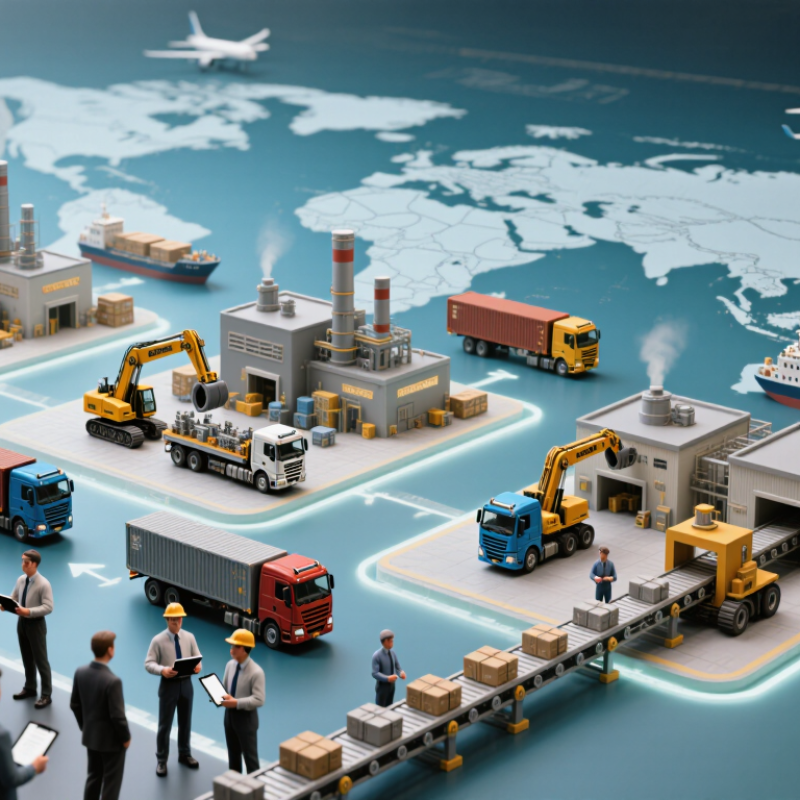
Vertical integration means owning or directly controlling more stages of production, from materials and components to assembly and distribution. In global manufacturing, buyers may integrate to secure critical inputs, protect production schedules, or improve quality oversight. A factory controlling its component supplier can trace a defect faster. But ownership is not automatically efficiency; it can also concentrate risk and tie up capital.
Seven checks can help buyers assess the fit. Map each production stage and identify bottlenecks, such as a single-source motor or a port-dependent shipment. Compare ownership with long-term contracts and qualified backup suppliers. Check whether local teams can manage different sites and time zones. Audit quality controls at every handoff. Keep clear specifications for parts made across regions. Model the costs of inventory, transport, and unused capacity. Set exit options if demand or technology changes.
The case for resilience is real, but integration is only one response. McKinsey & Company’s 2020 survey of supply-chain executives found that 93 percent planned to make their supply chains more resilient. That figure reflects executive intent, not proof that owning suppliers delivers better outcomes. Buyers should test assumptions against lead-time records, defect rates, and disruption scenarios. The uncomfortable question is whether a new owned facility solves a measured problem—or merely makes the supply chain look more controlled.
A useful vertical-integration decision starts with a stage map, not a list of suppliers. Trace a product from raw inputs through processing, component production, assembly, testing, packaging, and delivery. For each stage, record the facility location, lead time, capacity, owner, and information passed downstream. A cast housing, for example, may depend on a specific alloy, heat-treatment slot, and machining tolerance. That matters.
Map the dependencies between stages, including single-source materials, shared tooling, utilities, skilled labor, and transport lanes. Mark where one disruption could stop several production lines, rather than merely delay one shipment. Ask suppliers for evidence: recent capacity data, process-flow diagrams, change-control records, and recovery assumptions. Compare these records with purchase orders and observed delivery patterns. Spreadsheets can hide conflicting definitions of “available capacity.” Maps age quickly.
Use the map to decide what to own, what to contract, and where a backup source adds real resilience. A buyer might integrate a high-risk finishing step while keeping commodity packaging external. But ownership does not automatically remove dependency; a captive plant may still rely on imported controls or one experienced technician. Flag uncertain links openly, assign an owner to verify them, and refresh the map after product changes or recurring delays.
Map key supply-chain stages and dependencies before deciding what to produce in-house or source externally.
How to read this chart: The bars show midpoint planning estimates in days; the ranges below reflect typical variability, not guaranteed delivery times.
Raw materials: 60–90 days · Tier 2 components: 30–60 days · Tier 1 components: 14–30 days · Final assembly: 7–14 days · International transport: 20–40 days. Map each stage’s suppliers, capacity constraints, and handoffs, then validate lead times against your products and shipping lanes before making sourcing or integration decisions.
Global manufacturing buyers should assess make-or-buy decisions separately for each region. A component made in-house may look cheaper until local labor, energy, maintenance, and equipment costs are included. A supplier’s quote also needs context: freight, packaging, inspection time, and the cost of holding extra inventory can change the comparison. Maps can mislead. Two nearby facilities may face very different port access, power reliability, or skilled-labor availability.
In plant reviews, a useful starting point is a clear cost model built from actual production data, not broad regional averages. Compare unit cost, lead time, defect rates, and the time required to qualify a supplier. Then test what happens if demand rises, shipping slows, or a key input becomes harder to obtain. That matters. Keep sensitive processes in-house when control, process knowledge, or rapid design changes are central; outsource when capable local suppliers can meet documented quality requirements. The boundary is not always obvious. Early estimates can be too neat, especially when teams overlook training, tooling changes, or rejected batches. A small pilot run can expose those gaps before a major commitment, though pilots rarely capture every seasonal or operational constraint. Review the decision with local operations staff and revisit it when costs, capacity, or customer needs shift.
7 Vertical Integration Tips for Global Manufacturing Buyers
Coordinate Suppliers, Logistics, and Compliance
Tip 1: Build one shared production-and-shipping calendar. Ask suppliers to report material availability, production milestones, and booking deadlines in the same format. A delay in one component can leave a finished-goods order waiting beside a loading dock. The World Bank’s 2023 Logistics Performance Index reports that shipments spend an average of 44 days moving between export and destination ports, with about 60% of that time at ports and terminals. Plan buffer time around real shipping routes, not ideal schedules.
Tip 2: Link supplier records to shipment documents. Keep purchase orders, product descriptions, origin details, and required certificates consistent across teams. Have qualified local compliance staff review classification and destination requirements before goods ship. Small mismatches matter. A missing document can create costly holds, even when production is on time.
Tip 3: Set a weekly exception review with suppliers, freight partners, and internal compliance staff. Discuss late materials, changing routes, and incomplete paperwork using named owners and due dates. Track recurring causes, not just missed deadlines. This process is not foolproof; teams may still overlook quiet risks or rely too heavily on one supplier. That deserves regular reflection. Keep decisions and corrective actions in a shared audit trail, then revise the process when actual lead times differ from forecasts.
| No. | Integration Tip | Practical Actions | Primary Owner | Useful Measures and Records |
|---|---|---|---|---|
| 1 | Map the end-to-end supply chain | Document key materials, production sites, subcontractors, transport routes, border crossings, and delivery destinations. Identify single-source dependencies and critical handoffs. | Supply chain management | Approved supplier and site list; route map; single-source exposure; documented handoff points |
| 2 | Segment suppliers by risk and importance | Assess suppliers using factors such as supply criticality, geographic concentration, financial condition, quality history, and availability of qualified alternatives. Set review frequency according to risk. | Procurement and risk management | Supplier risk register; assessment date; corrective-action status; qualified alternative sources |
| 3 | Align forecasts, capacity, and purchase orders | Share rolling demand forecasts, confirm capacity and lead times, and distinguish forecast information from firm purchase commitments. Escalate material changes through an agreed process. | Planning and procurement | Forecast updates; confirmed capacity; supplier lead time; order changes; schedule adherence |
| 4 | Coordinate logistics from origin to destination | Agree shipment responsibilities, required shipping documents, packaging standards, delivery locations, and escalation contacts. Track shipment milestones and allow for customs clearance in transit plans. | Logistics and trade operations | On-time delivery; transit time; milestone visibility; document completeness; freight exceptions |
| 5 | Build trade compliance into purchasing | Establish processes to verify product classification, country-of-origin information, customs valuation, restricted-party screening, and applicable import or export controls. Retain supporting records. | Trade compliance | Classification records; origin documentation; screening logs; customs entries; audit findings |
| 6 | Link quality controls across supplier tiers | Define specifications, inspection and testing requirements, nonconformance reporting, and change-approval rules. Trace affected materials and production lots through relevant records. | Quality management | Incoming defect rate; supplier corrective actions; inspection results; lot traceability; approved changes |
| 7 | Prepare for disruptions and review performance | Set response plans for supplier outages, transport delays, port disruptions, and compliance holds. Review performance with suppliers regularly and assign owners and due dates to improvement actions. | Cross-functional operations team | Recovery plans; disruption response time; open action items; supplier review records; recovery test results |
Measure vertical integration by its operating results, not by how much production moves in-house. Track supplier lead times, defect rates, inventory days, and the cost per accepted unit. Track more than purchase price. Compare those figures with a clear pre-integration baseline, then review them monthly at the plant level. OECD analysis estimates that global value chains account for around 70% of international trade, so a disruption at one facility can affect several linked stages. McKinsey Global Institute’s 2020 report, “Risk, resilience, and rebalancing in global value chains,” estimates that companies may lose 45% of one year’s profits over a decade from supply-chain disruptions. These figures make recovery time worth tracking alongside efficiency.
Use the data to adapt the integration strategy, not just defend the original plan. If an internal component line cuts lead time but raises scrap rates, investigate the process before expanding it. A two-week pilot can reveal issues hidden by annual averages: a bottleneck at a heat-treatment station, for example, may erase savings elsewhere. Set review thresholds for cost, quality, and recovery time, and name who acts when results fall short. Keep at least one qualified external source where it protects flexibility. This is not always the cheapest choice. Recheck the assumptions when demand shifts, equipment ages, or a site repeatedly misses targets. Some measures will be imperfect; record the gaps and improve the next review.