How to Evaluate Instrument Finishing Craftsmanship?
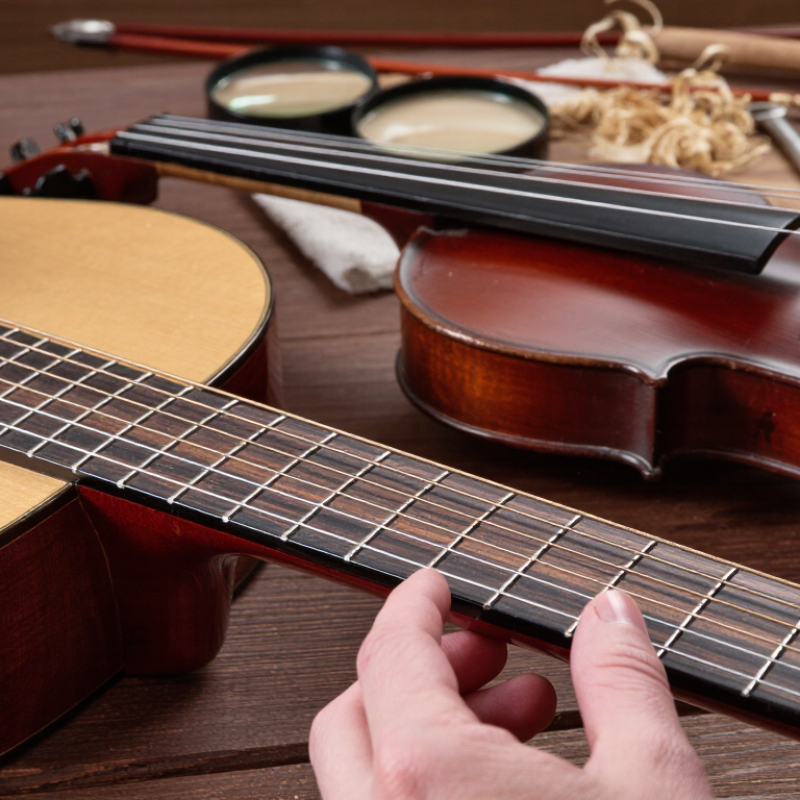
Instrument finishing craftsmanship is more than a glossy surface or an attractive color. It reflects the care taken to shape, join, seal, and inspect an instrument. Small details matter. On a guitar, for example, look closely at fret ends, binding edges, and the transition between the neck and body. On a violin, examine the varnish for even coverage without expecting every handmade surface to look identical. These visible details can reveal consistency, but they do not prove how well an instrument plays or will age.
A useful evaluation combines close observation with careful handling. View the finish under soft, angled light; it can reveal cloudy patches, scratches, uneven polish, or finish gathered around hardware. Run a clean finger gently along accessible edges to notice rough spots, and check that seams appear neat and stable. Avoid treating a mirror-like shine as a quality guarantee. A thin, even finish may show the maker’s work more clearly than a heavy coat, though materials and design affect what is appropriate. Listen to the instrument and assess its setup separately; finishing and performance are related, not interchangeable. Some marks may be harmless signs of handwork, while others deserve a closer inspection. That distinction is not always obvious. When uncertain, ask the maker or a qualified repair professional about the instrument’s materials, finish process, and care needs. A thoughtful assessment leaves room for doubt. Craftsmanship is best judged through several details, not one impressive photograph.
Identify the Finish System and Measure Coating Thickness under ISO 2808
How to Evaluate Instrument Finishing Craftsmanship?
Identify the finish system before judging its thickness. A clear lacquer, a pigmented coating, and a plated layer need different inspection approaches. Look closely at edges, screw holes, and curved surfaces, where uneven coverage can hide. Check for trapped dust, runs, pinholes, and a consistent sheen under angled light. Small flaws matter.
ISO 2808:2019 describes methods for determining coating film thickness, including approaches suited to different coating and substrate combinations. Choose a method that will not damage the instrument, and record where each reading was taken. Compare dry-film measurements with the finish specification; a thicker layer is not automatically better.
The 2016 IMPACT study by NACE International estimated global corrosion costs at US$2.5 trillion, or 3.4% of global GDP. This is a broad industry estimate, not an instrument-specific figure, but it underscores why coating performance deserves careful measurement. A measurement alone cannot reveal poor curing or weak adhesion.
Tips: Take several readings across flat areas and edges. Keep the gauge clean, verify its calibration, and note the finish system. If results vary, inspect again. The method may be part of the problem.
Compare Color Uniformity Using CIELAB ΔE00 (ISO/CIE 11664-6)
Color uniformity can be checked by comparing a finished instrument surface with an approved reference. CIELAB describes color through L* for lightness, a* for red–green, and b* for yellow–blue. ISO/CIE 11664-6 specifies the CIEDE2000 method, reported as ΔE00. Unlike a simple distance between coordinates, it adjusts for differences in lightness, chroma, and hue.
Use a calibrated spectrophotometer and keep its measurement geometry, aperture, and settings consistent. Take readings at several locations, such as the body’s center, edge, and near a curve. Record the reference and sample values under the same conditions. A lower ΔE00 generally indicates closer color agreement, but there is no single acceptance limit for every finish. Small differences matter.
Gloss, wood grain, and surface curvature can affect readings or make a patch appear different to the eye. Check for dust, fingerprints, and uneven lighting before measuring. A single reading can mislead. ΔE00 is useful evidence, not a full judgment of craftsmanship; it does not describe tactile feel, coating depth, or how the finish looks in changing light. If the numbers and visual inspection disagree, repeat the measurements and note the viewing conditions rather than forcing a convenient result.
How to Evaluate Instrument Finishing Craftsmanship?
Compare Color Uniformity Using CIELAB ΔE00 (ISO/CIE 11664-6)
Example inspection readings show ΔE00 color difference from a reference finish at five locations. Lower values indicate closer color agreement; the readings are illustrative and are not acceptance limits. Measure under consistent viewing and measurement conditions, and use ISO/CIE 11664-6 to calculate ΔE00.
Measure Surface Gloss in GU at 20°, 60°, or 85° (ISO 2813)
How to Evaluate Instrument Finishing Craftsmanship?
Measure Surface Gloss in GU at 20°, 60°, or 85° (ISO 2813)
A polished instrument finish should look consistent across curves, edges, and flat panels. Gloss units (GU) provide a repeatable way to describe that appearance. ISO 2813:2014 specifies specular-gloss measurement at 20°, 60°, and 85°. Its angle-selection guidance uses 60° as the general starting point, 20° for high-gloss surfaces above 70 GU at 60°, and 85° for low-gloss surfaces below 10 GU at 60°. These are measurement guidelines, not universal quality targets. A bright reflection can look impressive, yet reveal uneven sanding or tiny waviness when viewed at an angle.
For a useful comparison, clean the surface, keep the glossmeter flat, and measure several marked spots under consistent conditions. Record the angle, GU readings, and location; a single reading may hide variation between a body’s center and its curved edge. Small differences matter. Still, numbers cannot fully judge color depth, texture, or how a finish looks in ordinary room light. I would treat the reading as evidence, not a verdict.
Tips: Use the same instrument settings and surface locations each time. If 60° readings are near either selection threshold, check the suggested 20° or 85° geometry too. Keep a simple measurement log. It is easy to overlook a dusty patch, and even careful operators can disagree about which spots best represent the finish.
Rate Coating Adhesion on ISO 2409’s 0–5 Classification Scale
A clean-looking instrument finish can still fail at the cut. ISO 2409 checks coating adhesion by cutting a grid through the film to the substrate, then assessing detachment. Use the prescribed cutter spacing for the coating thickness, and keep the cuts even. Remove loose particles; apply tape only when the test procedure requires it. Small details matter.
The classification runs from 0 to 5. Grade 0 means the cut edges remain smooth, with no squares detached. Grade 1 allows tiny flakes at intersections, affecting less than 5% of the grid. Grade 2 indicates 5–15% loss; Grade 3, 15–35%; Grade 4, 35–65%; and Grade 5, more than 65%. Higher numbers mean poorer adhesion. Record the grade, coating condition, substrate, and test setup so another technician can interpret the result. Compare samples only when preparation and test conditions are consistent. A single rating is useful, but it does not explain why the coating lifted. I have seen an uneven cut complicate the reading; that is worth noting, not hiding. ISO 2409 provides a classification, not a direct measurement of bond strength.
How to Evaluate Instrument Finishing Craftsmanship? - Rate Coating Adhesion on ISO 2409’s 0–5 Classification Scale
Use the ISO 2409 cross-cut classification to describe coating separation around and between cuts. Lower ratings indicate better resistance to detachment. The affected-area ranges below are commonly used to interpret the classification; assess the cut area under consistent test conditions.
| ISO 2409 classification |
Approximate affected area |
Typical appearance after cutting |
Coating adhesion interpretation |
Finishing review |
| 0 |
0% |
Cut edges are smooth; no squares of the coating are detached. |
Best classification in this scale; no visible cross-cut detachment. |
Strong result for coating adhesion under the test conditions. |
| 1 |
Up to about 5% |
Small flakes detach at cut intersections; the affected area is limited. |
Very slight detachment. |
Minor damage; compare with the product specification and other test results. |
| 2 |
More than about 5% and up to about 15% |
Flaking occurs along cut edges and/or at intersections. |
Limited but noticeable detachment. |
Review process consistency and confirm whether this rating meets the acceptance criteria. |
| 3 |
More than about 15% and up to about 35% |
Partial or complete flaking is visible along cut edges and/or at intersections. |
Substantial detachment in the cross-cut area. |
Investigate surface preparation, coating application, and curing before acceptance. |
| 4 |
More than about 35% and up to about 65% |
Extensive partial or complete flaking occurs along cuts and across the grid. |
Poor resistance to detachment in the test area. |
Typically warrants corrective action and retesting against the applicable specification. |
| 5 |
More than about 65% |
Flaking exceeds the extent represented by classification 4. |
Worst classification in this scale; very extensive detachment. |
Treat as a significant adhesion failure and investigate before release. |
Test note: ISO 2409 is a cross-cut test that classifies resistance to separation; it does not provide a direct numerical measurement of adhesion strength. Select cut spacing and perform the test according to the coating thickness, substrate, and applicable edition of the standard. Record the substrate, coating thickness, cut spacing, test conditions, and rating. Use the result alongside other relevant inspection criteria when judging overall finishing craftsmanship.
Inspect Edges, Joints, and Curved Surfaces under Consistent Lighting
Good finishing is easiest to assess when the lighting stays consistent. Place the instrument beneath a bright, diffuse light, then inspect it from several angles without moving the light source. Reflections reveal more than color alone. A straight highlight should travel smoothly across a curved surface, without sudden ripples, cloudy patches, or tiny bumps. Check the body’s curves near the waist and edges, where sanding marks can hide in changing reflections. Look closely.
Run a clean fingertip gently along accessible edges. The transition should feel even, with no sharp spots, rough fibers, or thick finish ridges. At joints, examine the seam under the same light. A neat joint should look consistent and free of obvious gaps, excess finish, or abrupt color changes. Some materials and construction methods leave visible seams, so judge regularity rather than expecting every joint to disappear. Take your time. I’ve found that a quick glance can miss a flaw that becomes clear when the instrument is tilted slowly. Dust can also mimic a finish defect; wipe the surface with a soft, clean cloth and check again before deciding. A small imperfection may be worth noting, even when it does not affect playability.